Search News
TerraVista Metrics (TVM)Industry Portal
TerraVista Metrics (TVM)Hot Articles
TerraVista Metrics (TVM)- How to Plan Outdoor Kinetic Art Installations for Parks, Resorts, and Public SpacesOutdoor kinetic art planning guide for parks, resorts, and public spaces—explore safety, engineering, materials, lifecycle costs, and maintenance for lasting visitor impact.
- Amusement Equipment Testing for Family Entertainment Centers: Key Safety ChecksAmusement equipment testing for family entertainment centers: discover essential safety checks for restraints, brakes, interlocks, structural wear, and daily operations.
- What Engineering Performance Testing Should Cover During a Specification ReviewEngineering performance testing for specification review: learn how to verify structural strength, durability, safety, sustainability, and system reliability before costly project decisions.
Popular Tags
TerraVista Metrics (TVM)Industry NewsMaterial Performance Validation: Tests and Acceptance Criteria for Critical Parts
auth.Time
Sep 05, 2026Click Count
Material performance validation establishes whether a critical part can carry its intended load, resist its environment, retain its function through service, and remain within defined safety limits. For tourism infrastructure, hospitality equipment, attraction hardware, outdoor facilities, and modular structures, the decision cannot rest on a material name, a catalogue value, or a visually acceptable sample. A stainless-steel fastener, polymer enclosure, laminated panel, welded bracket, or upholstered seating frame may appear suitable while failing under corrosion, cyclic loading, cleaning chemicals, ultraviolet exposure, moisture migration, vibration, or repeated public contact.
A valid program begins with the actual duty condition. The part's material, geometry, joining method, finish, installation orientation, expected loading, maintenance exposure, and foreseeable misuse all affect the test plan. Material performance validation therefore links engineering requirements to inspection evidence and measurable acceptance criteria before parts are released for installation.
Define the Part as a Functional System
Testing a material coupon alone is often insufficient. Critical parts usually fail at interfaces: a bolt thread strips before a bracket yields; a coating cracks at a sharp edge; water enters through a seam; a composite panel delaminates around an insert; a connector loses retention after vibration. The validation record should identify the complete part configuration, including drawings, revisions, material grade, thickness, heat treatment where relevant, surface preparation, coating system, weld procedure, adhesive, hardware, and assembly torque.
Each requirement should be traceable to a functional hazard or service condition. For example, a handrail support on an elevated deck may require proof of static load capacity, resistance to repeated side loading, corrosion protection at cut edges, and secure anchorage into the host structure. A smart-room sensor enclosure may need impact resistance, flame-related performance where specified by the installation context, ingress protection appropriate to its location, dimensional stability, and compatibility with routine disinfectants. A component cannot be accepted simply because its base resin or metal grade is familiar.
Classify Failure Consequences Before Selecting Tests
Failure consequence determines the rigor of validation. Parts whose failure could lead to injury, loss of containment, fire spread, structural instability, electrical exposure, or an inaccessible evacuation route require stronger evidence than decorative trim. Classification should account for hidden failures as well as immediate breakage. A concealed anchor that progressively corrodes, a fatigue crack under a coating, or a foam layer that promotes moisture retention can create a significant defect long before it becomes visible.
A practical classification separates parts into categories such as life-safety, load-bearing, functional continuity, environmental containment, and appearance retention. A part may fall into more than one category. The assigned category should then determine sample selection, third-party test needs where applicable, inspection frequency, allowable deviations, documentation depth, and disposition authority for nonconforming results.
Build Acceptance Criteria Before the Test Starts
A test report is useful only when pass and fail conditions were defined in advance. Vague language such as “no significant damage” leaves too much room for interpretation. Acceptance criteria should specify the loading sequence, environmental conditioning, measurement method, permitted permanent deformation, allowed crack length if any, electrical or mechanical functionality after testing, and the visual inspection standard.
For structural and mechanical components, criteria may include proof load without fracture, a maximum residual deflection after unloading, absence of thread damage, no separation at joints, and continued operation of any moving mechanism. For seals and enclosures, criteria may include a defined ingress condition, no leakage at stated pressure or exposure duration, stable compression set within a project limit, and no loss of latch engagement. For finishes, criteria may address corrosion products, blistering, flaking, color change, gloss change, abrasion breakthrough, or coating adhesion after conditioning.
Acceptance limits must distinguish safety-related damage from cosmetic variation. A minor color variation in a concealed finish may be acceptable. A pinhole in a protective coating near a wet interface may not be. Photographs, reference panels, measurement locations, and calibrated gauges reduce disagreement during review.
Mechanical Strength, Fatigue, and Joint Integrity
Static strength testing verifies that a part can withstand a specified force or moment. It should reproduce the installed load path rather than applying force at a convenient laboratory location. Fixtures that artificially restrain rotation or distribute load more evenly than the field installation can create misleading results. The test setup should document support conditions, fastener grade, tightening method, substrate thickness, spacing, and any backing plate or reinforcement used in service.
Where a part experiences repeated use, cyclic testing is usually more revealing than a single overload test. Hinges, seat frames, gate latches, retractable barriers, deck connections, suspension elements, and moving attraction hardware can deteriorate through accumulated stress below the apparent static strength. The cycle profile should reflect load direction, rate, dwell time, impact potential, and the number of load reversals anticipated during the intended service interval. Inspection during cycling matters because loosening, fretting debris, audible cracking, heat generation, or increasing travel may precede final failure.
Joints deserve separate scrutiny. Welds should be evaluated for the applicable quality level, weld size, fusion, undercut, porosity, cracking, distortion, and accessibility for later inspection. Bolted assemblies require verified thread engagement, torque or tension control, locking method, bearing surface condition, and resistance to loosening under vibration. Bonded assemblies should be tested after moisture, heat, and chemical conditioning because adhesive strength measured immediately after cure may not represent long-term exposure.
Environmental Exposure Must Match the Installed Location
Material selection often fails when the service environment is simplified to “indoor” or “outdoor.” Covered outdoor areas can receive wind-driven rain and condensation. Coastal locations may deposit salt on sheltered surfaces. Poolside hardware encounters humid air and chemical residues. Mountain installations can combine freeze-thaw cycling, intense ultraviolet radiation, and abrasive grit. Interior parts near kitchens, spas, laundry areas, or entrance zones may face heat, steam, oils, detergents, or frequent cleaning.
Environmental conditioning should be selected from the credible exposure mechanism. Corrosion testing may involve cyclic wet-dry exposure, salt-containing atmospheres, crevice-prone assemblies, or dissimilar-metal contact rather than a single generic spray test. Polymer and composite parts may need ultraviolet exposure, temperature cycling, humidity conditioning, and post-conditioning tensile, impact, or flexural checks. Timber-based products may require moisture-content verification, swelling assessment, bond-line evaluation, and checks for coating failure around fasteners and cut ends.
Test duration alone does not establish equivalence to field life. Accelerated exposure is most useful when the failure mechanism is understood and the specimen construction represents production. A coated steel panel tested without edges, drilled holes, overlaps, or fasteners may demonstrate coating behavior but not the corrosion risk of the installed assembly.
Dimensional Control and Material Identity
Critical parts can fail because tolerances accumulated across fabrication and installation. A nominally compliant bracket may not seat flat, causing eccentric loading. An enclosure gasket may be compressed unevenly. A modular wall connection may lose fit after thermal movement. Dimensional inspection should therefore cover features that affect structural engagement, sealing, clearances, alignment, electrical spacing, and replaceability, rather than recording only overall length and width.
Material identity needs positive control where substitution would change performance. This can include incoming certificates, heat or batch traceability, marking verification, hardness checks, coating-thickness measurements, alloy verification where justified, and comparison against approved reference samples. Certificates should not be treated as conclusive when the delivered condition can differ from the documented source material through mixed stock, incorrect labeling, unauthorized substitution, damage during transport, or a changed fabrication process.
For polymers, fabrics, foams, laminates, and engineered wood, batch identification is equally important. Density, thickness, reinforcement orientation, moisture level, pigment, fire-retardant package, adhesive formulation, and cure conditions can influence results. Retaining representative samples from accepted production lots supports later investigation if field defects emerge.
Transport, Storage, and Installation Are Part of Validation
A part that passes factory testing may lose its performance margin before commissioning. Long modular panels can warp when stored without adequate support. Coated components can be scratched by unprotected stacking. Hygroscopic materials can absorb moisture in transit. Sensitive electronic housings can be damaged by impact or electrostatic handling. Packaging requirements should protect the part's critical surfaces and should be verified through handling conditions that resemble the actual logistics route.
Installation controls must identify conditions that invalidate the tested configuration. These can include drilling through protected surfaces, field welding near finished coatings, unsupported spans, incorrect anchor embedment, incompatible sealants, excessive fastening torque, missing isolation washers between dissimilar metals, or blocked drainage paths. The installation record should capture the essential variables, including substrate condition, anchor type, torque values where specified, weather limitations for coatings or adhesives, and final inspection points.
Field acceptance is not a duplicate of laboratory validation. It confirms that the delivered assembly matches the qualified design and that site conditions have not introduced a new risk. A limited proof test, functional cycling test, torque audit, continuity measurement, water test, or alignment check may be appropriate depending on the part's function.
Evidence Review and Release Control
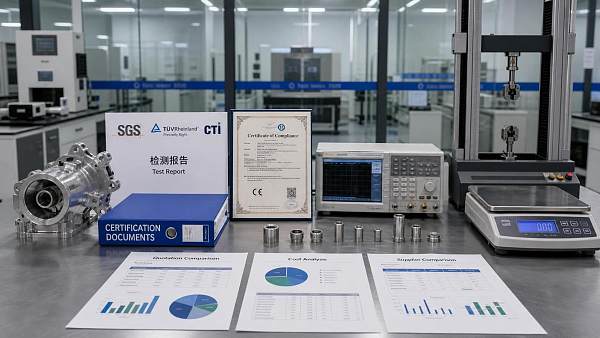
Material performance validation should produce a reviewable evidence package rather than isolated test certificates. The package normally links the requirement list to drawings, bill of materials, sample identification, test method, equipment calibration status, environmental conditioning, raw observations, deviations, photographs where needed, and final disposition. Results from a prototype should be clearly separated from evidence for serial production, particularly when tooling, source material, fabrication location, or assembly sequence has changed.
Nonconformities require technical evaluation, not automatic acceptance because a defect appears minor. The review should establish whether the deviation affects load capacity, fatigue resistance, corrosion protection, flame-related properties, sealing, electrical safety, maintenance access, or interchangeability. A corrective action is complete only when the revised part or process is assessed against the requirement that was missed. Rework can introduce its own risks, especially where grinding alters weld profiles, touch-up coatings leave edge gaps, or added shims change the load path.
Release criteria should also address ongoing conformity. A qualified first article does not guarantee that later deliveries retain the same properties. Changes in raw material source, thickness, coating supplier, cure schedule, weld consumable, molding parameters, fastening hardware, or subcontracted process should trigger a defined change review. The scope may range from document review and dimensional confirmation to repeat environmental or mechanical testing, depending on the effect on the validated characteristics.
Common Misjudgments in Critical-Part Assessment
- Accepting a high nominal strength value without checking the installed connection, load direction, and long-term fatigue condition.
- Using an environmental test on an ideal specimen to approve an assembly with cut edges, drainage traps, joints, and dissimilar materials.
- Treating a material certificate as evidence of final-part conformity after forming, welding, coating, transport, and field modification.
- Setting visual acceptance rules without defining measurement points, lighting conditions, reference samples, or the functional significance of the observed defect.
- Approving a substitute component because dimensions match while its stiffness, hardness, corrosion behavior, flame-related performance, or chemical compatibility differs.
The strongest validation records connect a specific part to a specific service condition and a measurable release decision. When requirements, specimens, tests, and installation conditions remain traceable, performance claims can be examined before they become maintenance issues, safety incidents, or costly replacement work.
Recommended News
 Sep 01, 2026How to Use a Tourism Standards Database to Verify Safety and Compliance RequirementsTourism standards database guide: verify safety, compliance, evidence scope, test conditions, and jurisdiction requirements with confidence.
 Aug 31, 2026Material Performance Validation: Tests and Acceptance Criteria for Critical PartsMaterial performance validation: discover essential tests and acceptance criteria that help critical parts withstand loads, corrosion, fatigue, and real-world service conditions.
 Aug 26, 2026What Is a CMS and How Do You Choose One for a Growing Business Website?CMS explained for growing business websites: learn how to choose a CMS that supports SEO, workflows, integrations, and long-term scalability without costly rebuilds.
 Aug 24, 2026How to Build a Technical Procurement Content Workflow for Faster Vendor EvaluationTechnical procurement content workflow strategies for faster vendor evaluation: standardize intake, compare evidence clearly, surface risks early, and cut costly procurement delays.
 Aug 20, 2026How to Evaluate Sustainable Concrete Alternatives for Low-Carbon Building ProjectsSustainable concrete alternatives: learn how to compare carbon data, structural performance, code compliance, and supply risk to choose low-carbon concrete solutions with confidence.
 Aug 17, 2026What Does Product Category Insights Reveal About Buyer Demand and Market Positioning?Product category insights reveal buyer demand, key product attributes, and market positioning. Learn how to spot reliable signals, compare segments, and make smarter decisions.
 Aug 13, 2026How to Use Industry Benchmarking to Improve Specification Planning DecisionsIndustry benchmarking for specification planning helps technical evaluators make smarter procurement decisions, reduce risk, and improve long-term performance with evidence-based standards.
 Aug 12, 2026Technical Certification Pricing Model: What Drives Cost and How to Compare QuotesTechnical certification pricing model explained: learn what drives cost, spot hidden risks in low quotes, and compare certification proposals with confidence before you approve budget.
 Aug 09, 2026How to Evaluate Tourism Equipment for Eco Resorts Without Compromising Guest ExperienceTourism equipment evaluation for eco resorts made practical: learn how to balance sustainability, durability, and guest comfort to avoid costly mistakes and choose smarter.
 Aug 07, 2026How to Evaluate LEED Standards for Environmental Sustainability in Building ProjectsEnvironmental sustainability assessment LEED standards explained: learn how to evaluate prerequisites, credits, costs, and project risks to achieve smarter, more reliable green building outcomes.
 Aug 05, 2026Why Eco Structures in the Middle East Are Shifting Toward Modular, Off-Grid DesignsEco structures in Middle East markets are moving to modular, off-grid designs for faster delivery, lower operating risk, and stronger climate resilience. Discover what is driving the shift.
 Jul 30, 2026Industry Insights for Market Expansion: How to Identify High-Potential Regions?Industry insights for market expansion: learn how to identify high-potential regions by assessing demand, infrastructure, compliance, and supply chain readiness for smarter growth.
 Jul 14, 2026How to Apply a Tourism Innovation Validation Framework to Assess New Visitor ProjectsTourism innovation validation framework explained: learn how to assess new visitor projects, reduce delivery risk, verify compliance, and make smarter investment decisions.
 Jul 13, 2026Import Market Research Checklist: How to Assess Demand, Tariffs, and Supplier RiskImport market research made practical: learn how to assess real demand, model tariffs, and reduce supplier risk with a clear checklist for smarter sourcing decisions.
 Jul 11, 2026Fade Resistant Durability: Which Test Methods Matter for Long-Term Outdoor Use?Fade resistant durability starts with the right test data. Discover which methods best predict long-term outdoor performance, color stability, and lower lifecycle risk.
 Jul 09, 2026Electronic Gadgets for Travel and Daily Use: How to Pick Features That MatterElectronic gadgets for travel and daily use should deliver real value. Learn how to compare battery life, portability, durability, and connectivity before you buy.
 Jul 08, 2026Regulatory Compliance Framework Explained: Core Elements, Gaps, and Audit ReadinessRegulatory compliance framework explained for modern organizations: learn core elements, common gaps, and audit readiness strategies to reduce risk, improve control, and strengthen decisions.
![]() Jul 07, 2026Faucets and Mixers Buying Guide: Types, Valve Options, and Finish SelectionFaucets and mixers buying guide covering fixture types, valve options, and finish selection. Compare durability, comfort, maintenance, and performance before you buy.
 Jul 06, 2026Tourism Equipment Specification Review: Which Ratings Matter Before You Buy?Tourism equipment specification review made practical: learn which ratings truly affect safety, lifecycle cost, compliance, and uptime before you choose a supplier.
 Jul 05, 2026What Is Material Fatigue in Composites? Failure Mechanisms and Service Life BasicsMaterial fatigue composites explained: learn key failure mechanisms, service life factors, and how to assess durability risks before specifying composite products.
 Jul 03, 2026Tourism Destination Infrastructure in North America: What Investors and Developers Evaluate FirstTourism destination infrastructure in North America shapes returns from day one. Discover what investors and developers assess first to reduce risk, improve resilience, and protect long-term value.
 Jul 02, 2026Tourism Development Validation Methodology Explained: Metrics, Data Sources, and Use CasesTourism development validation methodology explained with key metrics, trusted data sources, and real use cases to reduce risk, improve compliance, and guide smarter tourism investment decisions.
 Jun 30, 2026Regulatory Compliance Criteria Explained: How to Evaluate Requirements by Product and MarketRegulatory compliance criteria explained clearly: learn how to assess product and market requirements, reduce approval risk, and make smarter sourcing and market-entry decisions.
 Jun 29, 2026Efficient Procurement Planning: How to Reduce Delays and Control Budget RiskEfficient procurement planning helps reduce delays, control budget risk, and improve supplier decisions with data-driven strategies for stronger project delivery.
Quarterly Executive Summaries Delivered Directly.
Join 50,000+ industry leaders who receive our proprietary market analysis and policy outlooks before they hit the public library.