Search News
TerraVista Metrics (TVM)Industry Portal
TerraVista Metrics (TVM)Hot Articles
TerraVista Metrics (TVM)- Cloud Integration Interoperability Testing: Methods, Metrics, and Release GatesSystem interoperability testing cloud integration: explore practical methods, key metrics, and evidence-based release gates for secure, reliable connected operations.
- Hotel Security Protocols: A Compliance Checklist for Protecting Guests and StaffSecurity protocols for hospitality: use this practical hotel compliance checklist to protect guests, staff, data, access points, and emergency operations.
- How to Evaluate Resort Slide System Suppliers for Safety, Capacity, and Project SupportResort slide systems supplier evaluation guide: compare safety evidence, real capacity, durable materials, and project support for confident resort investments.
Popular Tags
TerraVista Metrics (TVM)Industry NewsPlastic Machinery Buying Guide: Key Machine Types, Output Needs, and Cost Factors
auth.Time
Sep 10, 2026Click Count
Why does plastic machinery selection matter so much at the buying stage?
Plastic machinery is rarely a simple equipment purchase. It shapes output stability, product quality, utility consumption, maintenance exposure, and payback speed.
That matters even more when capital projects depend on durable components, repeatable finishes, or high-volume plastic parts across construction, hospitality, leisure, and infrastructure supply chains.
In practical terms, the right machine is not always the fastest or cheapest one. It is the one that fits the product mix, resin behavior, staffing level, and planned operating window.
This is where many comparisons go wrong. Suppliers often emphasize maximum capacity, while actual buying decisions should focus on stable capacity under real material and tooling conditions.
For organizations working with performance-led procurement, the question is broader than machine output alone. Reliability, compliance, traceability, and lifecycle cost all carry weight.
That approach aligns with how TerraVista Metrics evaluates industrial inputs behind tourism infrastructure. The useful question is not just what a machine can produce, but whether it supports long-term asset quality.
Which plastic machinery types should be on the shortlist?
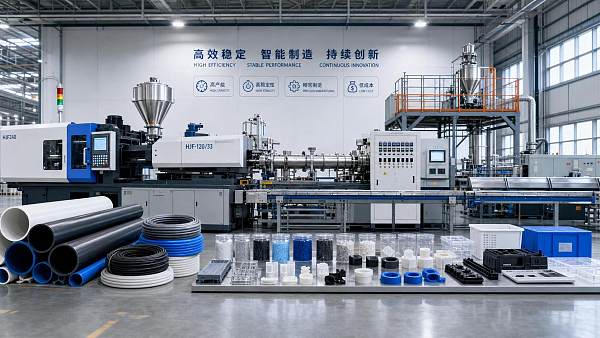
The answer depends on the part geometry, production scale, and finish requirement. Still, most plastic machinery buying decisions start with a few core machine families.
Injection molding machines
These are usually chosen for precise, repeatable parts with tighter tolerances. Housings, fittings, furniture parts, and smart system enclosures often fall into this category.
They work well when surface consistency matters and when multi-cavity tools justify higher tooling investment.
Extrusion lines
Extrusion plastic machinery suits continuous profiles such as pipes, sheets, films, edging, and insulation-related products. Output is often measured by kilograms per hour, not parts per cycle.
For projects involving modular structures or utility networks, extrusion often becomes more relevant than molding.
Blow molding equipment
When hollow products are required, blow molding enters the discussion. Containers, tanks, and certain leisure product shells are common examples.
Thermoforming systems
This machine type is often used for trays, liners, panels, and formed sheet products. It can be cost-effective for larger surface parts with lighter wall sections.
Recycling and compounding machinery
More buying teams now ask whether plastic machinery should support recycled content, regrind recovery, or custom material blending. That question affects both machine design and quality control needs.
A useful shortlist usually starts with process fit, then narrows by output range, utility demand, automation level, and supplier support depth.
How should output needs be calculated before comparing suppliers?
A common mistake is buying plastic machinery around peak claims instead of actual production planning. Real output needs should be based on saleable output, not theoretical output.
Start with the annual volume target. Then convert that number into shift hours, downtime assumptions, scrap allowance, changeover frequency, and maintenance windows.
For injection molding, part weight, cavity count, and cycle time drive the calculation. For extrusion, line speed, material density, and dimensional tolerance matter more.
Needless oversizing can raise capital cost, floor space demand, and energy use. Undersizing creates late deliveries, rushed tooling changes, and unstable quality during high-load periods.
More experienced buying teams also test output against product mix. A machine that looks efficient on one resin may struggle when switching to filled, recycled, or heat-sensitive materials.
- Define required saleable output per day, week, and season.
- Add scrap, startup loss, and tooling change time.
- Check whether quoted output uses your actual resin grade.
- Ask for performance at normal operating speed, not only peak speed.
- Confirm whether utilities can support the quoted production rate.
This discipline becomes especially relevant when plastic components support guest-facing assets, where inconsistent quality can damage both operations and brand perception.
What really drives the total cost of plastic machinery?
Machine price is only one layer. The full cost picture usually includes tooling, installation, power, compressed air, cooling, operators, spare parts, software, and expected downtime.
Energy use is often underestimated. A lower-priced machine may consume more power per kilogram or per molded part, which changes the long-term economics fast.
Automation is another cost lever. Robots, conveyors, feeders, blenders, and quality sensors add upfront expense, but they can reduce labor dependency and reject rates.
Then there is maintenance structure. Some plastic machinery is affordable to buy yet expensive to keep running because parts lead times are long or service capability is weak in the target region.
Imported machinery may also carry hidden costs through duties, freight volatility, commissioning delays, electrical adaptation, and documentation gaps.
A better comparison uses cost per acceptable part, or cost per operating hour, instead of headline price alone.
When do supplier claims deserve a closer look?
Any plastic machinery proposal deserves deeper review when the quoted output seems unusually high, energy consumption seems unusually low, or tooling compatibility sounds too broad.
The most reliable comparisons are based on documented test conditions. Resin type, ambient temperature, part geometry, operator skill, and automation level all influence actual performance.
It is also worth checking control platform quality. A machine may run acceptably today yet become difficult to maintain if its software interface, alarms, and spare parts chain are poorly supported.
For sectors tied to public-facing infrastructure, compliance matters too. Material traceability, electrical conformity, guarding, and safety documentation should not be treated as secondary paperwork.
TVM’s broader benchmarking perspective is useful here. The strongest sourcing decisions usually come from verified data, not presentation quality. That principle applies to plastic machinery as much as to built tourism assets.
- Request run data using comparable materials and products.
- Review reject rates, not just average output.
- Confirm local service contacts and spare part availability.
- Ask for utility consumption under production load.
- Check electrical, safety, and regional compliance records.
What does a practical buying checklist look like before final approval?
By this stage, the goal is not gathering more brochures. The goal is reducing decision uncertainty with a structured comparison.
Start by matching each plastic machinery option against a defined product family. Then compare throughput, reject exposure, maintenance assumptions, utility burden, and integration requirements.
If the machine will support components used in modular hospitality units, outdoor infrastructure, attraction systems, or commercial furnishings, include durability and compliance expectations early.
A disciplined final review often includes these checkpoints:
- Does the machine fit the actual resin and part portfolio?
- Is quoted output realistic after scrap and downtime?
- Are tooling, utilities, and automation fully costed?
- Can the supplier support installation, training, and service regionally?
- Do compliance documents match the target market and project standards?
- Is there a clear benchmark for acceptable part quality?
A sound plastic machinery decision usually comes from balancing machine type, real output needs, and full cost visibility rather than chasing one attractive specification.
Before moving forward, organize the decision around measurable requirements, comparable supplier data, and lifecycle assumptions. That creates a stronger basis for approval and a lower-risk implementation path.
Recommended News
 Sep 10, 2026How to Evaluate Resort Slide System Suppliers for Safety, Capacity, and Project SupportResort slide systems supplier evaluation guide: compare safety evidence, real capacity, durable materials, and project support for confident resort investments.
 Aug 27, 2026Hospitality Supplier Comparison: A Procurement Framework for Quality, Cost, and ReliabilityHospitality supplier comparison: evaluate quality, total cost, compliance, and service reliability to reduce procurement risk and protect guest experience.
 Aug 14, 2026Bedding Sets Wholesale: How to Choose the Right Supplier for Hotels and RetailersBedding sets wholesale for hotels and retailers: learn how to choose the right supplier for quality, compliance, and reliable delivery.
 Aug 11, 2026ITB China 2026 Closes With 900 Global ExhibitorsITB China 2026 closes with 900 global exhibitors from 85 countries, highlighting China’s growing role in tourism sourcing, travel tech, and cross-border supply chain opportunities.
 Aug 06, 2026How to Evaluate a Marine Hospitality Solutions Provider for Guest Experience and ROIMarine hospitality solutions provider evaluation starts with performance, not visuals. Learn how to assess guest experience, compliance, integration, and lifecycle ROI before you invest.
 Jul 20, 2026Supplier Capability Verification: How to Assess Quality, Capacity, and Delivery RiskSupplier capability verification helps buyers assess quality, production capacity, and delivery risk with a practical framework to reduce sourcing surprises and make smarter procurement decisions.
 Jul 14, 2026Global Sourcing Procurement Planning: Key Cost, Risk, and Lead-Time Factors to CompareGlobal sourcing procurement planning: compare total landed cost, lead-time reliability, compliance, and supplier risk to avoid hidden losses and make smarter sourcing decisions.
 Jul 12, 2026Hotel Furnishing for Guest Rooms: What to Check Before Comparing Suppliers and QuotesHotel furnishing for guest rooms: learn what to verify before comparing suppliers and quotes, from materials and compliance to lead times and lifecycle cost.
 Jul 09, 2026High-End Furniture Quotation Explained: What Drives Price and How to Compare OffersHigh-end furniture quotation explained: learn what drives price, how to compare offers, spot hidden risks, and choose durable, compliant value for hospitality projects.
 Jul 08, 2026How to Choose a Thermal Efficiency Testing Service Provider for Compliance and ROIThermal efficiency testing service provider selection affects more than compliance. Learn how to compare scope, reporting, and ROI to reduce risk, control costs, and choose with confidence.
![]() Jul 07, 2026How to Choose a Smart Home Devices Wholesale Supplier in China for Stable OEM OrdersSmart home devices wholesale supplier in China selection starts with OEM stability, compliance, and quality control. Learn how to avoid sourcing risks and secure reliable long-term orders.
 Jul 05, 2026How to Use Sourcing Guides Category Education to Compare Suppliers and Reduce Buying RiskSourcing guides category education helps buyers compare suppliers with real evidence, cut procurement risk, and evaluate compliance, durability, integration, and total cost with confidence.
 Jul 04, 2026Plastic Machinery Buying Guide: Key Machine Types, Output Needs, and Cost FactorsPlastic machinery buying guide covering key machine types, real output planning, and total cost factors. Compare suppliers smarter, reduce risk, and choose equipment that supports quality and ROI.
 Jul 03, 2026Metal Fabrication Processes Compared: Cutting, Bending, Welding, and When to Use EachMetal fabrication choices shape cost, strength, finish, and lead time. Compare cutting, bending, and welding to choose the right process for durable, efficient results.
 Jul 02, 2026Product Category ISO Standards: How to Check Compliance Requirements Before SourcingProduct category ISO standards are the first check before sourcing. Learn how to verify real compliance, reduce risk, avoid delays, and choose suppliers with confidence.
 Jul 01, 2026How to Use an Exporters Directory with Verified Suppliers for Safer Sourcing DecisionsExporters directory with verified suppliers: learn how to screen exporters, spot weak claims, reduce sourcing risk, and build a safer shortlist for smarter buying decisions.
 Jun 30, 2026CNC Machining Price Breakdown: What Drives Cost for Materials, Tolerances, and Volume?CNC machining price explained: see how materials, tolerances, and production volume affect cost, risk, and quote accuracy to help buyers source smarter and save more.
 Jun 29, 2026How to Evaluate a Technical Integration Solutions Provider for Multi-System ProjectsTechnical integration solutions provider selection starts with risk, not demos. Learn how to assess interoperability, security, compliance, and long-term reliability for multi-system projects.
 Jun 28, 2026Hospitality Equipment Comparison: What to Evaluate Before Buying for Hotels and ResortsHospitality equipment comparison for hotels and resorts: evaluate durability, compliance, integration, sustainability, and lifecycle cost before buying to avoid costly mistakes.
 Jun 24, 2026Trade Resources for Importers in China: How to Vet Suppliers and Compare TermsTrade resources for importers in China help you vet suppliers, compare terms, and uncover quality or compliance risks early for smarter, safer sourcing decisions.
 Jun 23, 2026How to Evaluate a Structural Steel Manufacturer for Quality, Capacity, and CertificationsStructural steel manufacturer evaluation guide: learn how to assess quality systems, production capacity, and certifications to reduce risk, avoid delays, and choose a supplier with confidence.
 Jun 22, 2026Supplier Capability Analysis: Which Metrics Matter Before You Approve a New Supplier?Supplier capability analysis helps you assess quality, delivery, compliance, and risk before approving a new supplier. Discover the key metrics that protect performance and support smarter procurement decisions.
 Jun 21, 2026How to Source Wholesale Home Goods: Product Categories, MOQs, and Supplier Red FlagsWholesale home goods sourcing made smarter: explore key product categories, realistic MOQs, and supplier red flags to reduce risk, control costs, and choose reliable partners.
 Jun 20, 2026How to Choose a Hospitality Furniture Supplier for Hotels, Resorts, and Glamping SitesHospitality furniture supplier selection impacts durability, compliance, sustainability, and guest experience. Learn how hotels, resorts, and glamping sites can compare suppliers with confidence.
Quarterly Executive Summaries Delivered Directly.
Join 50,000+ industry leaders who receive our proprietary market analysis and policy outlooks before they hit the public library.