Search News
TerraVista Metrics (TVM)Industry Portal
TerraVista Metrics (TVM)Hot Articles
TerraVista Metrics (TVM)- How to Plan Outdoor Kinetic Art Installations for Parks, Resorts, and Public SpacesOutdoor kinetic art planning guide for parks, resorts, and public spaces—explore safety, engineering, materials, lifecycle costs, and maintenance for lasting visitor impact.
- Amusement Equipment Testing for Family Entertainment Centers: Key Safety ChecksAmusement equipment testing for family entertainment centers: discover essential safety checks for restraints, brakes, interlocks, structural wear, and daily operations.
- What Engineering Performance Testing Should Cover During a Specification ReviewEngineering performance testing for specification review: learn how to verify structural strength, durability, safety, sustainability, and system reliability before costly project decisions.
Popular Tags
TerraVista Metrics (TVM)Industry NewsHow to Evaluate Powder Coated Cableway Systems for Corrosion Resistance and Service Life
auth.Dr. Julian Rossi (Aesthetic Materials Specialist)Time
Sep 05, 2026Click Count
What evaluators often get wrong about powder coated cableway systems
The phrase powder coated cableway systems sounds reassuring because it suggests a finished, protected product. In procurement practice, that phrase means very little unless it is tied to substrate type, pretreatment method, coating chemistry, film build, geometry, and the exposure class the system is expected to survive. A cableway structure can look clean and uniform on delivery and still fail early at edges, joints, weld zones, fixings, or water traps. For technical evaluation, appearance is not the starting point. Failure mode is.
That matters even more in tourism and leisure infrastructure, where cable-supported transport or access systems may operate in mountain climates, coastal air, humid forests, or mixed-use attractions with long idle periods and seasonal maintenance gaps. In those environments, corrosion is rarely a single-surface problem. It is a system problem involving coating continuity, metal preparation, drainage, mechanical damage, and maintenance discipline.
The first practical distinction is this: powder coating is a finishing process, not a durability guarantee by itself. Service life comes from the whole protection stack. If a supplier cannot explain that stack clearly, the risk is already visible.
What should be evaluated beyond the finish description
When a specification simply says “powder coated steel” or “outdoor powder coating,” it leaves out the variables that actually govern field performance. Evaluators should ask, at minimum, what the base metal is, whether the steel is galvanized before coating, what pretreatment is used before powder application, what powder resin family is selected, and how the assembly handles cut edges, bolted connections, cavities, and abrasion points.
For cableway systems, those details are not secondary. Towers, support frames, stations, access platforms, guard assemblies, carriers, and peripheral hardware do not all see the same stresses. Some parts are exposed primarily to UV and rainfall. Others face repeated contact, grit abrasion, cleaning chemicals, de-icing salts, or galvanic interaction at fasteners. A single coating approach across all parts may be convenient for manufacturing, but it is not always technically sound.
One common misunderstanding is to treat powder coating as interchangeable with paint. In service-life discussions, that shortcut is misleading. Powder coating can provide a durable and attractive barrier finish, but its corrosion performance depends heavily on pretreatment quality and edge coverage. Unlike a lab coupon with flat geometry, real cableway components include welds, corners, perforations, flanges, brackets, and enclosed sections. Those are the places where poor preparation and thin film distribution show up first.
Why substrate and pretreatment usually matter more than color or gloss
If the structure is carbon steel, the next question is whether the corrosion protection strategy is duplex, meaning zinc protection combined with an organic top layer, or whether the powder sits directly on prepared steel. In outdoor public infrastructure, that distinction has large implications for damage tolerance. A duplex system can continue offering protection even after local coating damage, while a single organic barrier relies much more on film integrity.
Pretreatment deserves the same level of scrutiny. Surface cleaning, conversion coating, and contamination control have direct influence on adhesion and underfilm corrosion resistance. If pretreatment is inconsistent, the coating may pass an initial visual inspection yet lose adhesion after thermal cycling, humidity exposure, or impact damage. Technical reviewers should therefore look for process documentation rather than generic claims such as “advanced pretreatment” or “outdoor-grade finish.”
This is where experienced evaluators separate cosmetic quality from engineered durability. A smooth surface tells you the applicator can produce a presentable finish. It does not tell you whether the pretreatment line is controlled, whether weld residues were removed properly, or whether sharp edges were rounded enough for adequate film build.
Standards are useful, but only if they match the service environment
Standards and test reports matter, but evaluators should read them carefully. Salt spray testing, humidity testing, adhesion testing, impact resistance, and accelerated weathering can all contribute useful information, yet none should be interpreted in isolation. A strong salt spray result on a test panel does not automatically predict long life on a complex fabricated structure installed near the sea or in a freeze-thaw environment.
For corrosion classification and paint-system context, ISO 12944 is widely referenced in industrial coating decisions. For powder coatings on galvanized or steel substrates, buyers may also encounter qualification frameworks and applicator quality schemes used in architectural or industrial finishing markets. These references help, but the key question is whether the tested system resembles the delivered system in substrate, pretreatment, dry film thickness, and expected exposure category.
Evaluators should be cautious when suppliers present a test standard name without the underlying test configuration or acceptance criteria. A report is only meaningful if you can tell what was tested, how it was prepared, and what constitutes pass or failure. The more severe the installation environment, the less useful vague compliance language becomes.
Service life is mostly lost at the details
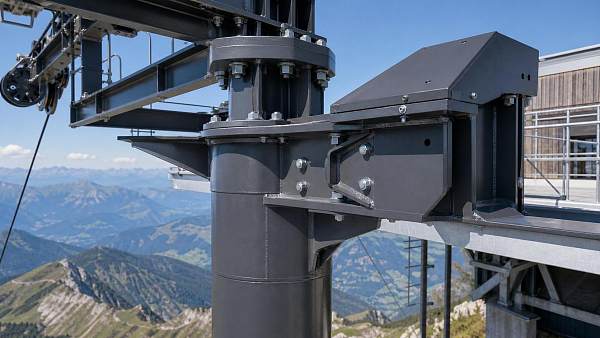
In real installations, corrosion rarely begins in the middle of an exposed flat member. It starts where the protective system is interrupted or strained: around bolt heads, at crevices between assembled parts, inside poorly vented sections, under clamps, beneath accumulated debris, or where maintenance access is weak. That is why a useful evaluation goes beyond material data sheets and asks how the structure is fabricated and assembled.
For cableway systems, vibration and routine mechanical contact also deserve attention. Boarding areas, maintenance zones, equipment housings, and transport interfaces can create repeated abrasion. If the finish is likely to be chipped by tools, harness hardware, cleaning equipment, or passenger contact, the repair strategy matters almost as much as the original coating build. Some systems are easy to touch up in a controlled way; others lose both appearance and corrosion protection once damaged.
Another point evaluators sometimes miss is the distinction between decorative weathering and structural corrosion risk. Chalking, gloss loss, and color fade may be acceptable in some noncritical peripheral parts, while blistering, underfilm rust creep, or failure around connections is not. A good specification separates aesthetic retention from structural protection instead of treating them as one issue.
How to read supplier claims with more discipline
Claims such as “marine-grade,” “heavy-duty outdoor,” or “long-life powder coating” should be treated as marketing shorthand until linked to verifiable system data. In a technical review, useful supplier evidence usually includes coating-system build-up, pretreatment route, dry film thickness range, adhesion or corrosion test references, and limitations on use conditions. If the supplier can only provide color charts and a general warranty statement, that is not enough for decision-grade evaluation.
Warranties also need context. A finish warranty may address appearance retention or localized corrosion under defined maintenance conditions, but it does not automatically cover operational downtime, inaccessible repairs, or corrosion at interfaces introduced during installation. For a cableway asset expected to remain in service for many years, lifecycle cost should include inspection frequency, touch-up procedures, coating compatibility for repairs, and the consequence of shut-down during refurbishment.
This is where independent benchmarking has practical value. The point is not to reject every supplier claim, but to normalize them into comparable engineering questions. What exactly was tested? Under which assumptions? On which substrate? With what maintenance interval? Once those questions are answered, selection becomes less subjective.
A workable decision framework for technical selection
A strong decision process usually starts with exposure mapping rather than product comparison. Identify whether the system will face coastal chlorides, industrial pollutants, high UV, persistent condensation, snow management chemicals, or frequent cleaning. Then match the coating strategy to that exposure, not the other way around.
After that, review the system through four lenses:
- Corrosion design: drainage, venting, edge treatment, joint design, accessibility for inspection.
- Protection stack: substrate, galvanizing or other metallic layer if used, pretreatment, powder chemistry, film thickness.
- Verification evidence: relevant standards, test reports, factory process control, batch inspection records.
- Maintenance reality: repairability, spare parts exposure, site-specific cleaning and inspection regime.
That framework is especially useful in destination infrastructure and attraction projects, where procurement teams often need to reconcile aesthetics, public safety, uptime, and total ownership cost. A coating system that looks premium on day one but requires complicated access equipment for routine touch-up may be the wrong choice even if the initial price is attractive.
What a defensible choice looks like
The best powder coated cableway systems are not defined by the word “powder coated.” They are defined by coherence between environment, material stack, fabrication detail, testing evidence, and maintenance plan. Technical evaluators should be able to explain why a given system is appropriate for a known exposure class, what its likely weak points are, and how those points will be managed over time.
If that explanation depends mostly on appearance, brochure language, or a generic outdoor claim, the assessment is too shallow. If it is grounded in substrate choice, pretreatment discipline, relevant corrosion testing, connection detailing, and realistic service access, the decision is on firmer ground. In this category, durability is rarely hidden in a single headline specification. It is usually visible in the details suppliers are willing, or unable, to disclose.
Recommended News
 Sep 04, 2026Planning Recreational Cable Transport Networks for Resorts and Mountain ParksExplore recreational cable transport networks for resorts and mountain parks, with expert planning insights on capacity, terrain, safety, station design, and long-term performance.
 Sep 02, 2026Mountain Slide Systems Pricing: Key Cost Factors for Resort ProjectsMountain slide systems pricing explained: explore key cost drivers for resort projects, from terrain and logistics to safety compliance, installation, and lifecycle planning.
 Jul 31, 2026How to Evaluate Powder Coated Cableway Systems for Corrosion Resistance and Service LifePowder coated cableway systems: learn how to assess corrosion resistance, pretreatment, substrate, and service life so you can choose safer, longer-lasting systems with confidence.
 Jul 26, 2026EN 13814:2026 Tightens EU Cableway Entry RulesEN 13814:2026 tightens EU cableway entry rules with mandatory AI monitoring and 100,000-cycle testing. Learn how manufacturers, operators, and importers should prepare now.
 Jul 18, 2026EN 13814:2026 Tightens EU Cableway Entry RulesEN 13814:2026 tightens EU cableway entry rules with new AI monitoring, wind load validation, and data interface demands. Learn what manufacturers, suppliers, and buyers must prepare now.
 Jul 17, 2026How to Choose Cableway Systems Equipment: Key Components, Load Capacity, and Safety StandardsCableway systems equipment selection starts with verified components, real load capacity, and safety standards. Learn how to compare systems and reduce long-term operational risk.
 Jul 16, 2026EN 13814:2026 Takes Effect for Cableway Tech ExportsEN 13814:2026 takes effect now, reshaping Cableway Tech exports to the EU with new wind-load and AI testing rules. Learn the compliance risks, certification impacts, and export steps companies should act on fast.
 Jul 12, 2026Recreational Cable Transport Market: Demand Drivers, Resort Use Cases, and Growth SignalsRecreational cable transport market trends are reshaping resorts and leisure destinations. Explore demand drivers, practical use cases, and the growth signals guiding smarter investment.
 Jul 05, 2026Performance Verification for Cableways: Test Items, Acceptance Criteria, and Safety ChecksPerformance verification for cableways explained: key test items, acceptance criteria, and safety checks to confirm readiness, reduce risk, and support reliable operation.
 Jun 26, 2026Cableway Compliance Analysis: How to Review Safety Standards, Documentation, and Risk GapsCableway compliance analysis helps review safety standards, documentation integrity, and hidden risk gaps—so you can strengthen compliance, reduce exposure, and support safer operations.
 Jun 25, 2026Durban Tourism Expo Signals New Cableway Entry RulesDurban Tourism Expo Signals New Cableway Entry Rules as South Africa and Rwanda buyers highlight ISO 18738, IEC 61508 SIL2, and third-party verification. See what suppliers must prepare now.
 Jun 25, 2026Recreational Cable Transport for Visitor Access: Key Safety and Capacity Factors to CompareRecreational cable transport for visitor access: compare safety, real capacity, evacuation readiness, and lifecycle reliability to choose a smarter, future-ready visitor mobility system.
 Jun 21, 2026EU Revises EN 13814:2026, Triggering New CertificationEN 13814:2026 revision brings new EU certification pressure for amusement rides and cableway systems. Learn the 2027 deadline, key testing changes, and how exporters can stay compliant.
 May 24, 2026France Launches 'Green Cableway' Tender Requiring EPDFrance’s 'Green Cableway' tender mandates EPD compliance—key for global suppliers. Act now to meet EN 15804 & 40% recycled material rules before the 30 June deadline.
 May 23, 2026France Announces €23B Africa Investment, Prioritizing Cableway Tech & Playground SafetyCableway Tech & Playground Safety take center stage in France’s €23B Africa investment—key opportunities for compliant exporters, certifiers, and contractors.
 May 22, 2026UIC Mandates OPC UA PubSub for Cableway Tech Maintenance InterfacesUIC mandates OPC UA PubSub for cableway tech maintenance—critical for EU market access. Learn compliance deadlines, impacted vendors, and urgent actions.
 May 21, 2026UIC Mandates OPC UA PubSub for Cableway SystemsUIC mandates OPC UA PubSub for cableway systems—learn how this binding 2027 standard impacts interoperability, cybersecurity, and real-time data in aerial transport.
 May 20, 2026UIC Mandates OPC UA PubSub for Cableway Tech InterfacesOPC UA PubSub is now mandatory for cableway tech interfaces per UIC’s 2026 mandate — ensure compliance, avoid bid disqualification, and future-proof your ropeway systems.
 May 20, 2026UIC Mandates OPC UA PubSub for Cableway AI-Ops InterfacesUIC mandates OPC UA PubSub for Cableway AI-Ops interfaces—unlock ultra-low latency, real-time edge diagnostics & future-proof AI-driven operations.
 May 19, 2026UIC Mandates OPC UA for AI-Based Cableway MaintenanceOPC UA is now mandatory for AI-based cableway maintenance per UIC’s new global standard — discover compliance deadlines, impacted industries, and actionable next steps.
 May 18, 2026UIC Mandates OPC UA for Cableway AI OperationsUIC mandates OPC UA for cableway AI operations—learn how this binding 2027 regulation impacts exporters, integrators, and suppliers globally.
 May 17, 2026UIC Mandates OPC UA for Cableway AI Ops Starting Oct 2026UIC mandates OPC UA for cableway AI ops from Oct 2026—critical for Chinese exporters, integrators & stack providers targeting EU, Japan & Chile markets.
 May 16, 2026UIC Mandates OPC UA AI Maintenance Interfaces for CablewaysUIC mandates OPC UA AI maintenance interfaces for cableways—learn how v2.1 impacts OEMs, control systems & certification globally.
 May 14, 2026UIC Releases Cableway Tech Standard Mandating Open AI Predictive Maintenance APIsUIC 650-2:2026 mandates open AI predictive maintenance APIs for cableway systems — a must-read for manufacturers, integrators & AI platform providers entering European and global markets.
Quarterly Executive Summaries Delivered Directly.
Join 50,000+ industry leaders who receive our proprietary market analysis and policy outlooks before they hit the public library.